In short
An AQL chart turns lot size into a code letter, then into a sample size with accept and reject numbers. At General Level II, 3,201 to 10,000 garments means inspecting 200: AQL 2.5 accepts up to 10 major defects and rejects at 11; AQL 4.0 accepts 14 minor defects and rejects at 15. Critical defects are normally zero.
Want a costing for your own style? Send us your enquiry
An AQL chart turns two facts, the size of your lot and the AQL you agreed, into three numbers: how many garments to inspect, how many defects you can accept, and the count at which the lot fails. For most apparel at General Inspection Level II, a lot of 3,201 to 10,000 pieces means inspecting 200 garments; at AQL 2.5 the lot passes with 10 major defects or fewer and fails at 11. At AQL 4.0 the same 200 pieces may carry 14 minor defects and fail at 15. Jump to the AQL 2.5 table.
What does AQL 2.5 actually mean?
AQL stands for Acceptance Quality Limit. It is the index that selects a sampling plan from the tables in ISO 2859-1, which uses the same tables as the American ANSI/ASQ Z1.4. The US National Institute of Standards and Technology describes the AQL as the baseline quality requirement for the producer’s product: a percent defective the process should be able to stay under.
So “AQL 2.5” is not a promise that 2.5% of your garments will be faulty, and it is not a guarantee that only 2.5% are. It is a rule for a decision. You draw a random sample of a fixed size, count what you find, and compare the count with an accept number and a reject number. Apparel orders usually carry two limits at once: 2.5 for major defects and 4.0 for minor defects, with critical defects set at zero. The quality control page explains how we apply those limits on an order. This article is about reading the chart itself.
Step 1: how do you find the sample size code letter?
The first table converts lot size into a code letter. The lot is the quantity presented for inspection, normally the whole order for one style from one factory. Pick the row for your lot size, then the column for your inspection level. Level II is the default unless the buyer specifies otherwise.
| Lot size (pieces) | Level I | Level II | Level III |
|---|---|---|---|
| 2 to 8 | A | A | B |
| 9 to 15 | A | B | C |
| 16 to 25 | B | C | D |
| 26 to 50 | C | D | E |
| 51 to 90 | C | E | F |
| 91 to 150 | D | F | G |
| 151 to 280 | E | G | H |
| 281 to 500 | F | H | J |
| 501 to 1,200 | G | J | K |
| 1,201 to 3,200 | H | K | L |
| 3,201 to 10,000 | J | L | M |
| 10,001 to 35,000 | K | M | N |
| 35,001 to 150,000 | L | N | P |
| 150,001 to 500,000 | M | P | Q |
| 500,001 and over | N | Q | R |
Read from Table I of MIL-STD-105E, the military standard these tables come from. The rows from 91 to 150,000 pieces were checked row by row on 23 September 2026, and the rows for smaller and larger lots on 1 October 2026. The letter is not a sample size yet. It is a pointer into the second table.
Step 2: the AQL 2.5 table, with sample size and accept and reject numbers
Print it: the AQL 2.5 table as a one-page PDF (A4), with AQL 1.5 and 4.0 alongside, free to print and share.
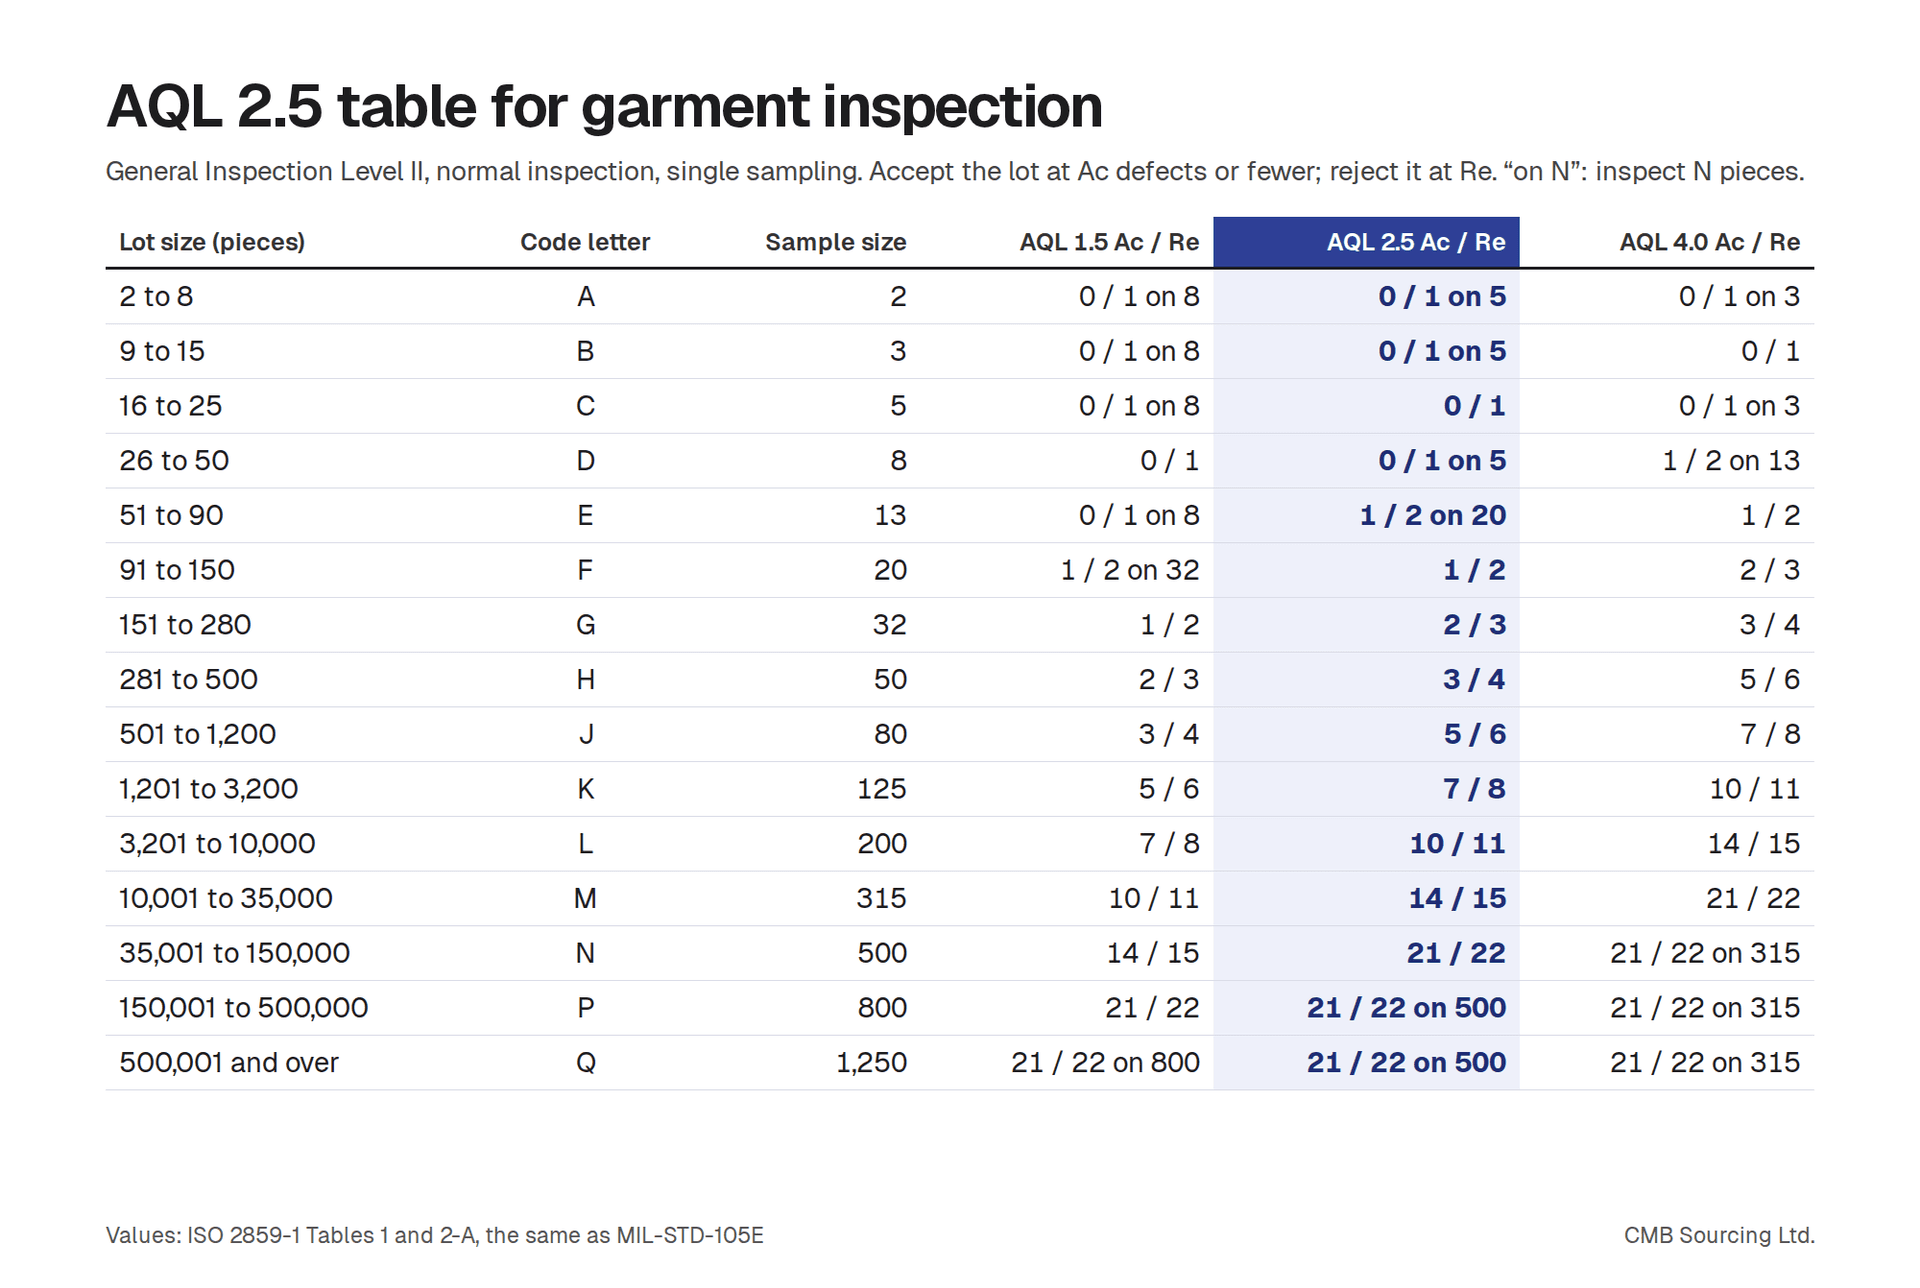
The second table, single sampling plans for normal inspection, gives each letter a sample size and, under each AQL column, an Ac (accept) and Re (reject) number. If the defects found are equal to or below Ac, the lot is accepted. If they reach Re, it is rejected. In the normal single sampling table there is no grey zone: Re is always Ac plus one.
| Lot size (Level II) | Code letter | Sample size | AQL 1.5 Ac / Re | AQL 2.5 Ac / Re | AQL 4.0 Ac / Re |
|---|---|---|---|---|---|
| 2 to 8 | A | 2 | 0 / 1 on 8 | 0 / 1 on 5 | 0 / 1 on 3 |
| 9 to 15 | B | 3 | 0 / 1 on 8 | 0 / 1 on 5 | 0 / 1 |
| 16 to 25 | C | 5 | 0 / 1 on 8 | 0 / 1 | 0 / 1 on 3 |
| 26 to 50 | D | 8 | 0 / 1 | 0 / 1 on 5 | 1 / 2 on 13 |
| 51 to 90 | E | 13 | 0 / 1 on 8 | 1 / 2 on 20 | 1 / 2 |
| 91 to 150 | F | 20 | 1 / 2 on 32 | 1 / 2 | 2 / 3 |
| 151 to 280 | G | 32 | 1 / 2 | 2 / 3 | 3 / 4 |
| 281 to 500 | H | 50 | 2 / 3 | 3 / 4 | 5 / 6 |
| 501 to 1,200 | J | 80 | 3 / 4 | 5 / 6 | 7 / 8 |
| 1,201 to 3,200 | K | 125 | 5 / 6 | 7 / 8 | 10 / 11 |
| 3,201 to 10,000 | L | 200 | 7 / 8 | 10 / 11 | 14 / 15 |
| 10,001 to 35,000 | M | 315 | 10 / 11 | 14 / 15 | 21 / 22 |
| 35,001 to 150,000 | N | 500 | 14 / 15 | 21 / 22 | 21 / 22 on 315 |
| 150,001 to 500,000 | P | 800 | 21 / 22 | 21 / 22 on 500 | 21 / 22 on 315 |
| 500,001 and over | Q | 1,250 | 21 / 22 on 800 | 21 / 22 on 500 | 21 / 22 on 315 |
Figures read from Table II-A of MIL-STD-105E, the master table of single sampling plans for normal inspection. The rows from 91 to 35,000 pieces were checked on 23 September 2026, and the other rows on 1 October 2026. Where the printed table has an arrow, the cell shows the plan the arrow points to and that plan’s sample size: “0 / 1 on 8” means inspect 8 pieces, accept none and reject at 1, and if that sample is as large as your lot, inspect every piece. We have reproduced the table, not calculated it. Always confirm against the table your inspector or your retailer’s manual uses.
A worked example: 2,400 hoodies at AQL 2.5 and 4.0
Say one style of hoodie, 2,400 pieces, made in one factory, is ready for final inspection at General Level II with AQL 2.5 major and 4.0 minor.
- Code letter: 2,400 falls in 1,201 to 3,200, so Level II gives K.
- Sample: K means 125 pieces, drawn at random across colours, sizes and cartons.
- Majors at AQL 2.5: accept with 7 or fewer, reject at 8.
- Minors at AQL 4.0: accept with 10 or fewer, reject at 11.
- Criticals: one is enough to reject.
The two counts are judged separately. Six majors and eleven minors fail the lot on minors, even though the majors passed. Six majors and ten minors pass both. A lot can fail on a single critical defect, such as a broken needle point, whatever the other two counts say.
Notice what the chart does not do. It does not scale neatly with quantity. A lot of 1,201 pieces and a lot of 3,200 pieces both get a sample of 125. That is deliberate: the tables protect the buyer more on larger lots, where the sample is a smaller share but the evidence is stronger.
Why AQL 2.5 is not a 2.5% defect allowance
A claim still repeated on inspection and sourcing websites is that AQL 2.5 lets 2.5% of the order be defective. The standard behind the chart says otherwise. MIL-STD-105E, a US military standard dated 10 May 1989, is the last revision of the standard that, as MIL-STD-105D, was adopted as ANSI Z1.4 in 1971 and, with minor changes, as ISO 2859 in 1974; NIST notes that the basic tables of the three remain the same. It is no longer a current standard: Notice 1 cancelled it on 27 February 1995 and referred future purchases to ANSI/ASQC Z1.4-1993. We quote it because it is free to read, but a purchase order or quality manual should cite the current standard, ISO 2859-1:2026 or ANSI/ASQ Z1.4. Its clause 3.1 defines the AQL, when a continuous series of lots is considered, as the limit of a satisfactory process average. Clause 4.4.2 adds that selecting or using an AQL does not give the supplier the right to supply any defective unit.
The accept number shows the same thing. At General Level II, a lot of 3,201 to 10,000 garments is code letter L: 200 are inspected, and at AQL 2.5 the lot passes with up to 10 major defects and fails at 11. Ten in 200 is 5% of the sample, twice the figure on the label. At Level III the same lot is letter M: 315 inspected, accept 14, reject 15, so up to 4.4% of the sample.
Clause 3.1 also warns that the AQL alone does not give the chance of accepting any single lot; for that you read the operating characteristic curve of the plan. MIL-STD-105E prints those values, and for this lot size they show how often a worse lot still passes.
| Lot of 3,201 to 10,000 pieces, AQL 2.5, normal inspection | Level II (letter L) | Level III (letter M) |
|---|---|---|
| Garments inspected | 200 | 315 |
| Accept / reject | 10 / 11 | 14 / 15 |
| Most defects that can pass, as a share of the sample | 5.0% | 4.4% |
| Passes 95 times in 100 when this share of the lot is defective | 3.08% | 2.94% |
| Passes 50 times in 100 when this share of the lot is defective | 5.33% | 4.66% |
| Passes 10 times in 100 when this share of the lot is defective | 7.7% | 6.4% |
Figures from Tables II-A, VI-A, X-L-1 and X-M-1 of MIL-STD-105E, checked 23 September 2026. The last three rows are the share of garments in the whole lot with a defect of the class being counted; the standard gives the same values for defects per 100 garments. Clause 3.1 explains the pattern: a plan is built to accept the great majority of lots when the process average is no worse than the AQL, which is why, under Level II, a lot more than twice as bad as the label, at 5.33% defective, still passes half the time. Level III costs 115 more garments to inspect and lowers each of the last three figures.
What this changes on a single order
Clause 1.2 of MIL-STD-105E says the plans are meant mainly for a continuing series of lots, and that anyone inspecting an isolated lot should consult the operating characteristic curves to find a plan with the protection they want. Clause 4.11 sets out how: choose a limiting quality, the defect level you want accepted only rarely, and a consumer’s risk, commonly 10% or 5%, then take the plan from Tables VI and VII. NIST describes the buyer’s side of the same trade-off as the lot tolerance percent defective (LTPD), a defect level the consumer finds unacceptable and wants accepted only with a low probability. ISO 2859-1:2026 lists tables of consumer’s risk quality (CRQ) in its contents; ask your inspector to use them when an order is a one-off.
- First or one-off order: decide the share of defective garments you are not willing to see pass more than 1 time in 10, and check that the level and AQL in your purchase order deliver it. If 7.7% at Level II is too high, choose Level III or a tighter AQL before production, not after a disappointing report.
- Defects found in the sample: ask for every defective garment the inspector finds to be repaired or replaced, even when the lot passes. Clause 4.4.2 supports that position.
- Repeat orders: because the AQL describes a process average, keep the defect counts from every inspection and compare them order by order, using the same defect classification and inspection checklist each time.
Want every order checked like this?
We check quality on the line and run an AQL final inspection before shipment, and you receive the report. Tell us what you want to make.
What do the arrows mean, and what about small lots?
Some cells in the printed table hold an arrow instead of numbers. That happens where the sample for that letter is too small to support the chosen AQL. The instruction printed with the table is to use the first sampling plan the arrow points to, and to use that plan’s sample size as well as its numbers. If the sample size then equals or exceeds the lot, inspect every piece.
This is why small orders feel expensive to inspect. A lot of 120 pieces at Level II needs 20 garments checked, a sixth of the order. For runs made through a small-run route, a buyer can accept that proportion, or check every piece of a first order and move to sampling once the factory has earned it.
Level I, II or III: which inspection level should you use?
ISO 2859-1 offers three general levels. Level II is the default. Level I inspects fewer pieces and discriminates less; Level III inspects more and discriminates more. On a lot of 3,201 to 10,000 pieces, the choice changes the sample from 80 (Level I, letter J) to 200 (Level II, letter L) to 315 (Level III, letter M).
The table also has four special levels, S-1 to S-4, with much smaller samples. Clause 4.9.1 of MIL-STD-105E says they may be used where relatively small samples are necessary and large sampling risks can or must be tolerated. In apparel they suit checks that cost a garment or a lot of time per piece, such as a full measurement check against every point on the spec or a destructive seam test, where a small sample is agreed in advance.
A careful buyer changes the level for a reason and writes it into the order: Level III on a first order with a new factory, or a tighter AQL of 1.5 on majors for a premium product.
Tightened, reduced and skip-lot inspection
AQL tables were designed for a continuing series of lots from one producer, not a single shipment. The introduction to ISO 2859-1 says the scheme protects the buyer by switching to tightened inspection when quality deteriorates, and rewards consistent quality by switching to a smaller sample. MIL-STD-105E sets the trigger in clause 4.7.1: tightened inspection starts when 2 out of 2, 3, 4 or 5 consecutive lots are rejected on original inspection.
- Normal: where every relationship starts, and the table above.
- Tightened: stricter acceptance criteria, used after repeated failures until quality recovers.
- Reduced: smaller samples after a run of accepted lots and steady production, at the discretion of the buyer or its quality team.
- Skip-lot: inspecting only randomly chosen lots once a producer is qualified. This is new in the 2026 edition.
For a brand placing two or three orders a year, the switching rules rarely come into play. They matter once you run repeat programmes with the same factory, and they are a good reason to keep inspection records in one place.
Did ISO 2859-1:2026 change the AQL chart?
ISO published a third edition, ISO 2859-1:2026, which cancels and replaces the 1999 edition. Its foreword lists the main changes: a new procedure for switching to skip-lot inspection, guidance on qualifying producers and products for it, guidance on randomly selecting lots, and the removal of the printed operating characteristic curves in favour of methods to construct them. The code letters and the acceptance tables are not in that list of changes.
So a chart printed from the 1999 edition still gives the same answers for normal single sampling. What changes is the paperwork: new contracts and quality manuals should cite the 2026 edition, and anyone offering skip-lot inspection should be able to show how they qualified the factory for it.
Five mistakes people make reading the chart
- Treating two factories as one lot. The standard applies to lots from one producer using one process; different producers are sampled separately.
- Counting defects when you meant defective pieces. The standard supports both nonconforming items and nonconformities per 100 items. Agree which one the report will count: a shirt with three faults is one defective piece but three defects.
- Sampling from the top cartons. The sample must be random across the lot, or the statistics mean nothing.
- Inspecting before the goods exist. Clause 4.5.2 of MIL-STD-105E lets the sample be drawn after every unit in the lot has been assembled, or during assembly only if the lot size is fixed before the first sample unit is drawn.
- Agreeing an AQL without defining a major. The chart counts; it does not classify. Classification lives in your tech pack and defect list.
What to do next
For Level I or III, or for an AQL of 0.65, 1.0 or 6.5, our AQL sample size calculator reads the sample size and the accept and reject numbers from the same table for any lot size.
Put the inspection standard, level and AQLs in the purchase order before production, next to the sealed sample and the measurement tolerances in your tech pack. If you are producing hoodies, t-shirts or anything else in Bangladesh and want the inspection plan agreed before a single piece is cut, see how we work or send us your quantities and style list and we will set out the sample sizes that apply.
Questions buyers ask.
What does 2.5 AQL mean in garment inspection?
It means the sampling plan is chosen from the AQL 2.5 column of the ISO 2859-1 or ANSI/ASQ Z1.4 tables, which in apparel is normally applied to major defects. It is not permission for 2.5% of the order to be faulty. MIL-STD-105E, the military standard these tables come from, defines the AQL as the limit of a satisfactory process average over a continuous series of lots (clause 3.1), and says that using an AQL gives the supplier no right to supply any defective unit (clause 4.4.2). In practice it selects an accept and a reject number. On a lot of 3,201 to 10,000 pieces at General Level II, you inspect 200 garments and accept with 10 major defects or fewer, which is 5% of the sample; 11 rejects it. At Level III the sample is 315, accepting 14 and rejecting at 15. Minor defects are counted separately, usually at 4.0, and critical defects are normally set at zero.
Is there an AQL chart for garment inspection as a PDF?
Yes. The free source is MIL-STD-105E, a US military standard of 10 May 1989 approved for public release. It was cancelled in 1995 in favour of ANSI/ASQC Z1.4, but NIST notes that the basic tables are the same, and a scanned copy is what we checked this article against. Inspection firms publish their own charts too, so compare them with the standard first. The official standard itself is sold by ISO and national standards bodies, and the current edition is ISO 2859-1:2026. Whichever copy you use, check three things before you rely on it: that it is the normal inspection table and not tightened or reduced, that it shows both general and special inspection levels, and that it prints the arrow instruction for empty cells. Then keep the same copy for the whole relationship with a factory, and attach it to your quality manual, so the inspector, the factory and your team are all reading identical numbers.
Should I use AQL 1.5, 2.5 or 4.0 for clothing?
The common apparel setting is General Inspection Level II with 2.5 for major defects and 4.0 for minor defects, and critical defects at zero. A tighter 1.5 on majors makes sense for premium products, for a first order with a new factory, or where a retailer’s quality manual demands it. On a lot of 3,201 to 10,000 pieces, moving majors from 2.5 to 1.5 cuts the accept number from 10 to 7 on the same 200-piece sample, so a factory needs visibly better workmanship to pass. Tighter limits cost more than inspection fees: expect more rework, and possibly higher prices from factories that price in the risk of failing. Loosening to 4.0 on majors is rarely worth it for branded clothing, because every major defect is a garment a customer might return. Whatever you choose, write it into the purchase order before production begins.
How do you read an AQL 2.5 table for garment inspection?
You read it in two steps: the lot size gives a code letter, and the code letter gives the sample size plus an accept and a reject number under the AQL 2.5 column. First, find your lot size in the code letter table and read across to your inspection level, normally General Level II. Then take that letter to the single sampling table for normal inspection. Take 2,400 hoodies of one style: 2,400 falls in 1,201 to 3,200 pieces, so Level II gives letter K. K means 125 garments, drawn at random across colours, sizes and cartons. Under AQL 2.5 the lot passes with 7 major defects or fewer and fails at 8; under AQL 4.0, minors pass at 10 and fail at 11. Each count is judged separately, and one critical defect rejects the lot. If a cell shows an arrow, use the first plan it points to, including its sample size. Confirm figures against your inspector’s table.
What is the difference between inspection levels I, II and III in AQL?
They set how many garments are inspected: Level I checks fewer pieces and discriminates less, Level II is the default, and Level III checks more and discriminates more. These are the three general levels in ISO 2859-1. The level changes the code letter, and the letter sets the sample. On a lot of 3,201 to 10,000 pieces, Level I gives letter J and 80 garments, Level II gives L and 200, and Level III gives M and 315. At AQL 2.5, Level II accepts up to 10 major defects and Level III up to 14, so a passing sample can be at most 5.0% defective, against 4.4%. The extra 115 garments buy protection: Level II passes a lot that is 7.7% defective 10 times in 100, while Level III gives those odds only to a lot 6.4% defective. Special levels S-1 to S-4 use far smaller samples for slow or destructive checks. Write your level into the purchase order.
What is the AQL 2.5 sample size at Level II for a garment order of 1,000 or 5,000 pieces?
At General Inspection Level II, a lot of 501 to 1,200 garments, such as 1,000, is code letter J: inspect 80 pieces, accept with 5 major defects or fewer at AQL 2.5, and reject at 6. A lot of 3,201 to 10,000 garments, such as 5,000, is letter L: inspect 200, accept 10 and reject at 11. For minor defects at AQL 4.0, the same samples accept 7 and reject at 8, and accept 14 and reject at 15. The sample does not scale neatly with quantity: every lot from 1,201 to 3,200 pieces gets 125, letter K. These are normal single sampling plans from Tables I and II-A of MIL-STD-105E, whose basic tables are the same as those of ISO 2859-1 and ANSI/ASQ Z1.4. Confirm them against the table your inspector or retailer’s manual uses.
Did ISO 2859-1:2026 change the AQL tables used for garment inspection?
No: the code letters and acceptance tables are not among the changes ISO lists for its third edition, ISO 2859-1:2026, which cancels and replaces the 1999 edition. The foreword lists four main changes: a new procedure for switching to skip-lot inspection, guidance on qualifying producers and products for it, guidance on randomly selecting lots, and the removal of the printed operating characteristic curves in favour of methods to construct them. So a chart printed from the 1999 edition still gives the same answers for normal single sampling. What changes is the paperwork: new purchase orders and quality manuals should cite the 2026 edition, and anyone offering skip-lot inspection should be able to show how they qualified the factory for it.
What are tightened, reduced and skip-lot inspection in AQL sampling for clothing?
They are the switching rules that adjust inspection to a factory’s record: tightened inspection uses stricter acceptance criteria after repeated failures, reduced inspection uses smaller samples after a run of accepted lots, and skip-lot inspection checks only randomly chosen lots once a producer is qualified. Every relationship starts at normal inspection. MIL-STD-105E clause 4.7.1 starts tightened inspection when 2 out of 2, 3, 4 or 5 consecutive lots are rejected on original inspection, and it continues until quality recovers. Reduced inspection follows steady production and is at the discretion of the buyer or its quality team. Skip-lot is new in the 2026 edition of ISO 2859-1. For a brand placing two or three orders a year the rules rarely come into play; they matter on repeat programmes with one factory, which is a good reason to keep inspection records in one place.
Which AQL inspection plan should I use for a one-off or first clothing order?
For a single, isolated lot, choose the plan by the protection it gives rather than by the AQL label: decide the share of defective garments you are not willing to see pass more than 1 time in 10, and check that the level and AQL in your purchase order deliver it. MIL-STD-105E clause 1.2 says the plans are meant mainly for a continuing series of lots, and clause 4.11 sets the method for an isolated lot: choose a limiting quality and a consumer’s risk, commonly 10% or 5%, then take the plan from Tables VI and VII. ISO 2859-1:2026 lists consumer’s risk quality (CRQ) tables in its contents, so ask your inspector to use them. Make the choice before production, not after a disappointing report, and ask for every defective garment found in the sample to be repaired or replaced, even when the lot passes.
How many garments are inspected on a small clothing order at AQL 2.5?
At General Level II, a lot of 91 to 150 garments is code letter F: inspect 20 pieces, and at AQL 2.5 accept 1 major defect and reject at 2. Smaller lots can need a larger share inspected: a lot of 51 to 90 is letter E, with a sample of 13, but at AQL 2.5 the printed table holds an arrow that points to the plan for 20 pieces, accept 1 and reject at 2, and you use that plan’s sample size as well as its numbers. If the sample then equals or exceeds the lot, inspect every piece. This is why small orders feel expensive to inspect: a lot of 120 pieces needs 20 checked, a sixth of the order. A buyer can accept that proportion, or check every piece of a first order and move to sampling once the factory has earned it.
Sources
Checked . Rules and figures change, so confirm anything that affects your pricing.
- ISO 2859-1:2026 sample pages via iTeh Standards: third edition (2026-01) replaces the 1999 edition; list of main changes; switching rules purpose; one producer, one process; nonconforming items vs nonconformities; contents list consumer’s risk quality (CRQ) tables (opens in a new tab)
- NIST/SEMATECH e-Handbook of Statistical Methods, section 6.2.2: definitions of the AQL (baseline requirement for the producer’s product), the lot tolerance percent defective (LTPD), producer’s and consumer’s risk and the operating characteristic curve (opens in a new tab)
- US Department of Defense: MIL-STD-105E, Sampling Procedures and Tables for Inspection by Attributes (10 May 1989, approved for public release), clauses 1.2, 3.1, 4.4.2, 4.5.2, 4.7.1, 4.9.1 and 4.11; Table I code letters, Table II-A normal single sampling, Table VI-A limiting quality at 10% acceptance, Tables X-L-1 and X-M-1 operating characteristic values (scanned copy) (opens in a new tab)
- NIST/SEMATECH e-Handbook of Statistical Methods, section 6.2.3.1: MIL-STD-105D adopted as ANSI Z1.4 in 1971 and, with minor changes, as ISO 2859 in 1974; MIL-STD-105E issued 1989; the basic tables remain the same (opens in a new tab)
- US Department of Defense: MIL-STD-105E Notice 1 (27 February 1995), cancelling MIL-STD-105E and referring future acquisitions to ANSI/ASQC Z1.4-1993 (scanned copy) (opens in a new tab)