In short
Colour fastness testing checks how well a garment’s colour survives washing, rubbing, light, sweat and water. Labs use the ISO 105 series and grade results from 1 to 5 on grey scales, or 1 to 8 for light. Standards set no pass marks; buyers write their own, often using OEKO-TEX STANDARD 100 staining limits as a floor.
Want a costing for your own style? Send us your enquiry
Colour fastness (colorfastness in US spelling and in AATCC method titles) is how well a garment’s colour survives washing, rubbing, light, sweat and water without fading or staining other fabrics. Labs test it with the ISO 105 series (or AATCC methods in the US) and grade the result on a grey scale from 1 (poor) to 5 (no change), except light fastness, which uses a 1 to 8 blue wool scale. The tests are standard; the pass levels are not. Buyers set them in their own quality standard, and OEKO-TEX STANDARD 100 publishes a public minimum for staining that many use as a floor.
What does colour fastness measure?
ISO 105-A01, the general principles part of the series, defines colour fastness as the resistance of a textile’s colour to the agents it meets during manufacture and use. Each test produces two kinds of result:
- Change in colour: how much the tested fabric itself faded or shifted.
- Staining: how much colour moved onto an undyed adjacent fabric or rubbing cloth.
Other visible changes, such as shrinkage or a change in surface gloss, are reported separately and are not part of the fastness grade. A report that says “colour fastness: pass” without the two grades and the method number is not much use to a buyer. Our guide to garment lab testing in Bangladesh lists the accredited labs there and what else a usable report must show.
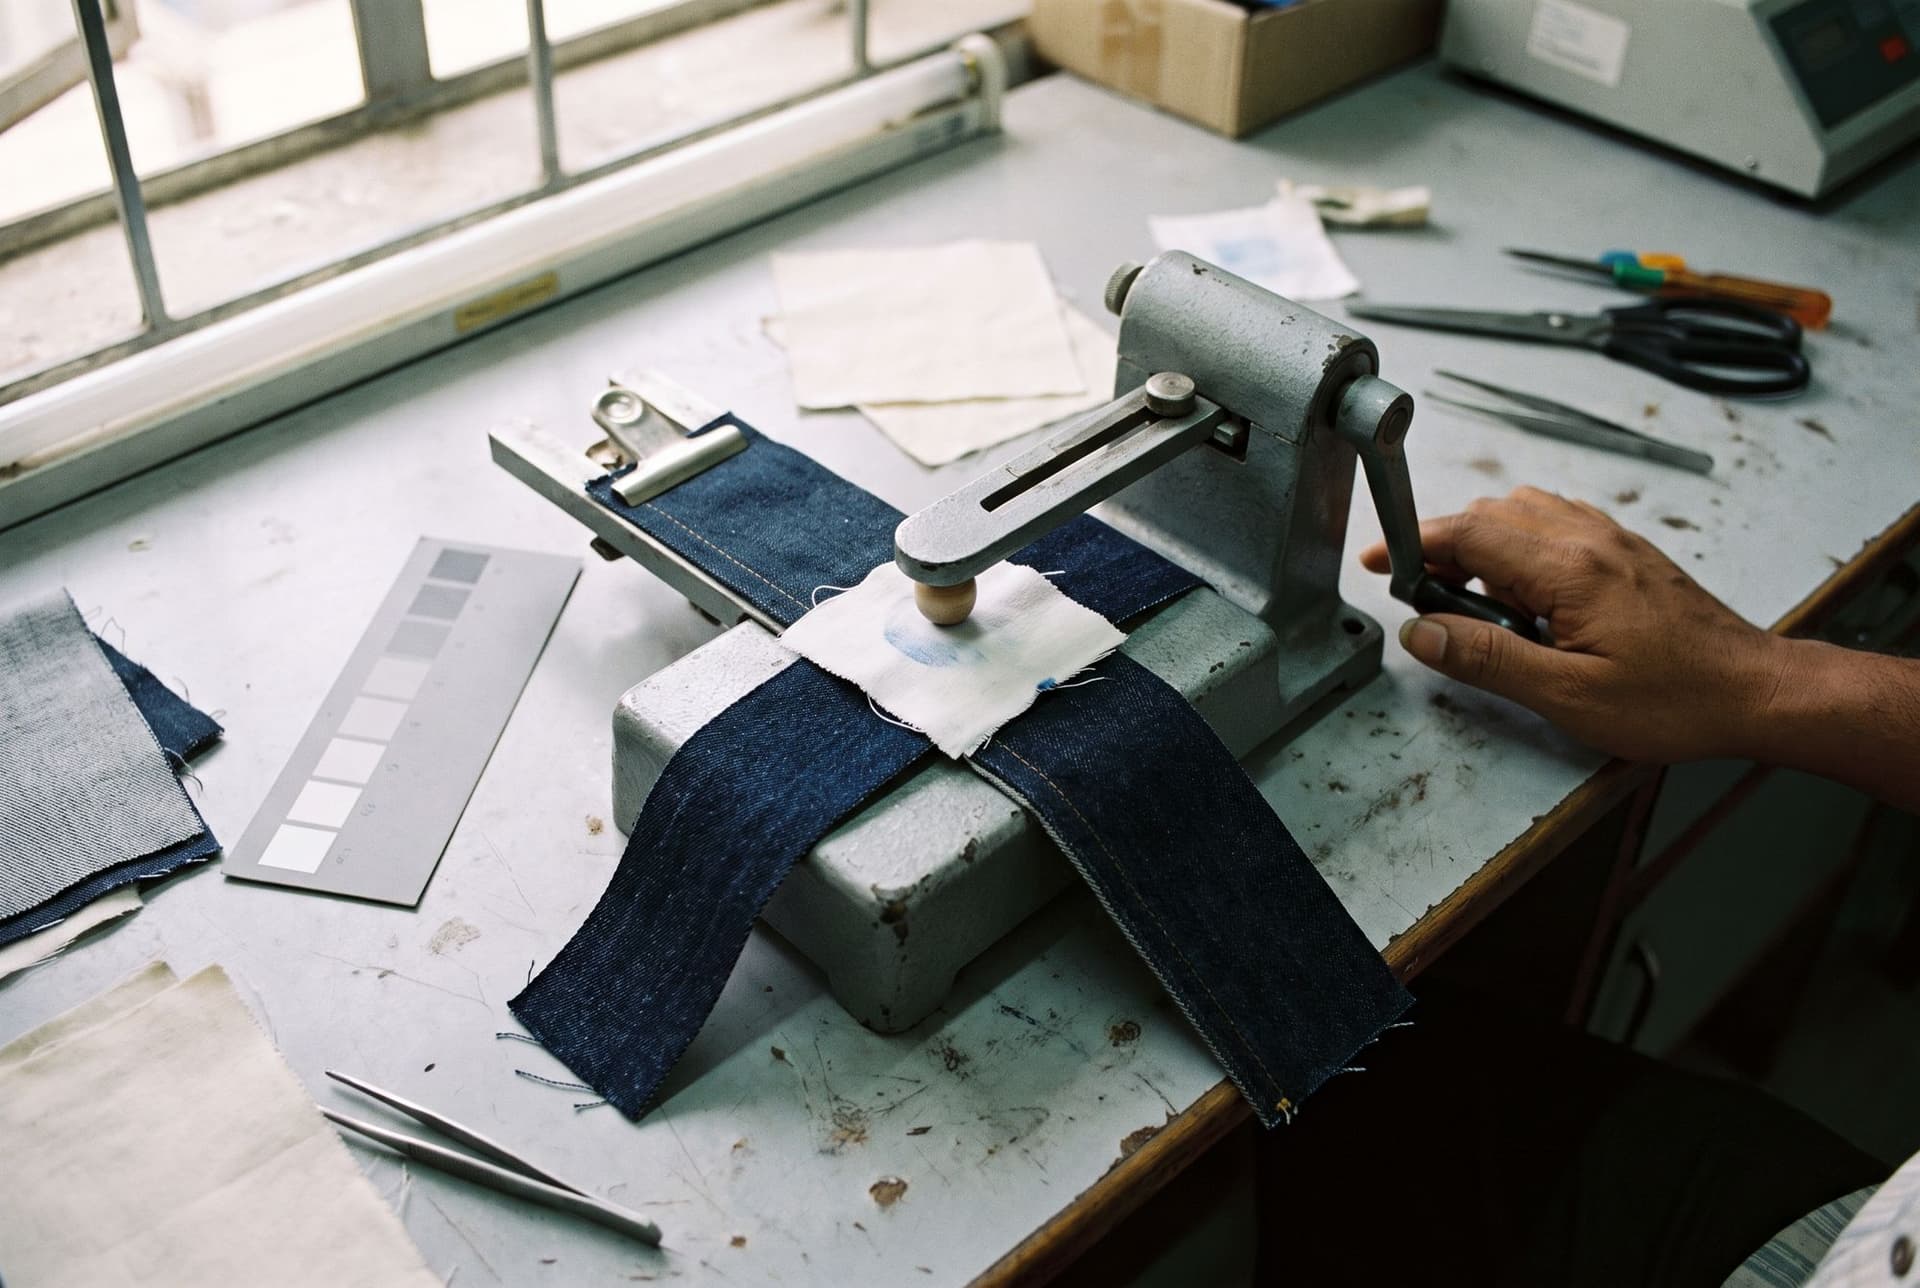
How the grey scale works: grades 1 to 5
Two grey scales do the grading. ISO 105-A02 assesses change in colour, and ISO 105-A03 assesses staining. Each is a set of paired grey or white chips. The technician compares the difference between the tested and untested fabric with the difference between the chips, under standard light, and picks the closest pair.
James Heal, which makes grey scales for testing labs, describes the ISO 105-A03 staining scale as nine pairs of chips running from grade 1 to grade 5, with four half steps. So the possible grades are 1, 1-2, 2, 2-3, 3, 3-4, 4, 4-5 and 5. Grade 5 means no visible change or staining. Grade 1 means severe change. Instrumental assessment with a spectrophotometer is also recognised in the series, which removes some of the judgement between two labs.
Light fastness uses a different scale entirely, graded against blue wool references, so a “4” for light is not the same as a “4” for washing.
The main colour fastness tests for clothing
| Test | ISO method | Nearest AATCC method | What it simulates | What is graded |
|---|---|---|---|---|
| Washing | ISO 105-C06 | TM61, laundering: accelerated | Domestic or commercial laundering with a reference detergent | Colour change and staining on a multifibre fabric |
| Rubbing (crocking) | ISO 105-X12 | TM8, crocking: crockmeter | Colour rubbing off onto other surfaces, dry and wet | Staining of the rubbing cloth |
| Light | ISO 105-B02 | TM16.3, light: xenon arc | Daylight, using a xenon arc lamp | Fading against blue wool references |
| Perspiration | ISO 105-E04 | TM15, perspiration | Acid and alkaline sweat | Colour change and staining |
| Water | ISO 105-E01 | TM107, water | Contact with water | Colour change and staining |
| Chlorinated pool water | ISO 105-E03 | TM162, water: chlorinated pool | Pool water: 50 or 100 mg/l active chlorine for swimwear, 20 mg/l for beach robes and towels | Resistance of the colour to active chlorine |
| Saliva | DIN 53160, with ISO 105-A03 and E04 | — | Babies mouthing fabric | Whether any colour transfers |
US buyers may write AATCC methods instead of ISO ones. The principle is the same, but the procedures differ, so a result under one family does not replace a test under the other. Name the exact method in the specification.
Colour fastness to washing: ISO 105-C06
ISO 105-C06 tests a specimen stitched to a multifibre adjacent fabric in a closed container with detergent solution and stainless steel balls about 6 mm across, which add mechanical action. According to the standard, one single (S) test closely approximates one domestic or commercial laundering. One multiple (M) test may approximate up to five launderings at temperatures not exceeding 70 °C, and is more severe because of the extra mechanical action.
The adjacent fabric matters. For tests at 40 °C and 50 °C the standard uses a multifibre strip that contains wool and acetate. For some 60 °C tests and all tests at 70 °C and 95 °C it uses a strip without them, because hot bleach can damage wool. The standard also allows two single-fibre adjacent fabrics instead, one of them the same fibre as the garment. With a multifibre strip, the staining grade is reported for each fibre, so one report can show a very different grade on two stripes of the same strip. Read the lowest grade, not the average: that is the fibre most at risk in your customer’s mixed laundry.
Ask the lab which adjacent fabric it used. Two reports for the same fabric, one on a multifibre strip and one on single-fibre fabrics, are not directly comparable, and suppliers sometimes send whichever looks better.
Choose the test code to match the care label. A garment labelled for 30 °C should not be judged on a 60 °C test, and a garment labelled for 60 °C must not pass only because it was tested at 40 °C.
Colour fastness to rubbing: ISO 105-X12
ISO 105-X12 rubs a white cotton cloth over the fabric with a crockmeter, once dry and once wet. Gester, an instrument maker, summarises the key settings as a downward force of 9 N, a 104 mm stroke and a 16 mm rubbing finger for ordinary fabrics. The staining on each rubbing cloth is graded on the ISO 105-A03 grey scale.
Deep shades are where rubbing complaints come from: black, navy and red jeans or sweatshirts that mark a white sofa or a light bag strap. That is why both the dry and the wet result belong in the specification. OEKO-TEX STANDARD 100 accepts a lower dry rubbing grade of 3 for pigment, vat and sulphur colourants instead of its usual 4, which tells you those colourant types are known to struggle here. If your range includes pigment-dyed or sulphur-dyed garments, agree the rubbing grade before bulk production, not after.
Not sure which fabric to choose?
Send a garment you like or describe the feel you want. We propose fabrics that suit the product, its price and your market.
Colour fastness to light: ISO 105-B02
ISO 105-B02 exposes the fabric to a xenon arc lamp representing natural daylight (D65), alongside blue wool references. The standard allows two sets of references: 1 to 8, preferred in Europe, and L2 to L9, preferred in America, and it states that results from the two sets are not interchangeable. On the European set, reference 1 has very low light fastness and reference 8 very high, and each step is roughly twice as fast as the one before. So the gap between grade 3 and grade 5 is about four times the exposure, not a small difference.
The test chamber’s humidity also changes the result, which is why the standard controls it with a humidity-test fabric. When you compare light fastness from two suppliers, make sure both labs used the same reference set and exposure conditions.
Light fastness matters most for outerwear, swimwear, caps, curtains and anything displayed in a shop window. For underwear or socks it is often a lower priority than washing and perspiration.
Perspiration, water and saliva
ISO 105-E04 soaks the fabric in artificial perspiration, in acid and alkaline versions, then presses it against adjacent fabric under load. Activewear, shirts and anything worn close to the skin in heat need this test. ISO 105-E01 does the same with water, which catches dyes that bleed when a garment is left damp.
For babywear, OEKO-TEX STANDARD 100 adds a saliva and perspiration test with reference to DIN 53160. If you sell kidswear, plan for it from the first lab dip.
What pass levels do buyers require?
ISO and AATCC do not set pass marks. The nearest thing to a public benchmark is OEKO-TEX STANDARD 100, whose February 2025 limit values include colour fastness to staining:
| Test (staining) | Class I, baby | Class II, skin contact | Class III, no skin contact |
|---|---|---|---|
| Water | 3-4 | 3 | 3 |
| Acid perspiration | 3-4 | 3-4 | 3-4 |
| Alkaline perspiration | 3-4 | 3-4 | 3-4 |
| Rubbing, dry | 4 | 4 | 4 |
| Saliva and perspiration | Fast | Not required | Not required |
Source: OEKO-TEX STANDARD 100 limit values, edition 02.2025. For pigment, vat or sulphur colourants, dry rubbing of 3 is accepted.
Two gaps are worth knowing. OEKO-TEX grades staining only, not colour change, and it does not set limits for washing fastness, wet rubbing or light. Those levels come from the brand’s own quality manual. If you do not have one yet, write the method, the test code, and a minimum grade for each of colour change and staining, and ask the lab to report grades, not just pass or fail. Our certifications page explains which certificates partner factories can show and how to check them.
Dark shades, reactive dyes and garment-dyed goods
Most failures come from unfixed dye left in the fabric. On cotton, reactive dyes bond to the fibre, but any dye that did not react must be washed off. Cotton Incorporated’s printing bulletin describes a quick in-plant check: take a washed sample before drying, lay it face down on white fabric and press with a hot iron for 10 seconds. The white should stay clean. It is not a substitute for a lab report, but it is a useful question to ask a dyehouse.
Garment dyeing adds risk because the dye goes into the finished garment, seams and threads included. The garment dyeing and washing method explains how we handle it. As a rule, test every colour separately, not just the darkest one, and retest when the dye lot changes.
Putting colour fastness into your specification
- List each test by its method number and test code, and the minimum grade for colour change and for staining.
- Match the washing test temperature to the care label.
- Require wet and dry rubbing results for dark and bright shades.
- Test at lab dip approval, on bulk fabric before cutting, and on finished garments if they are washed or dyed after sewing.
- Keep the reports with the purchase order so every repeat is tested to the same standard.
- Decide in advance what happens when a lot fails: re-treatment or re-dyeing by the mill, a retest at a named laboratory, and who pays for each. Agreeing this before production is far easier than arguing about it with goods waiting at the port.
Add these lines to the testing page of your tech pack. Ask for the test reports before shipment, and for shade and colour transfer to be checked at the final inspection that our quality control service runs. To agree test requirements for a new range, send us your specification.
Questions buyers ask.
What is a good colour fastness grade?
On the grey scale, 5 means no change and 1 means severe change, with half grades in between, so a higher grade is always better. There is no universal pass mark, because it depends on the test and the product. A useful public reference is OEKO-TEX STANDARD 100, which requires staining grades of at least 3 for water, 3-4 for perspiration and 4 for dry rubbing on garments worn against the skin, with stricter water results for baby items. It does not set washing, wet rubbing or light fastness limits, so brands add their own. Light fastness is graded differently, from 1 to 8 against blue wool references, so a light result of 4 is moderate rather than good. Always read the grade alongside the method and test code, because the same fabric can score differently at 40 °C and 60 °C.
How do you test colour fastness to washing?
The usual international method is ISO 105-C06. A specimen of the fabric is sewn to a multifibre strip containing several undyed fibres, then agitated in a closed container with a reference detergent solution and stainless steel balls at a set temperature and time. The test code picks the temperature and severity. A single (S) test approximates one home or commercial wash, while a multiple (M) test may approximate up to five washes at no more than 70 °C. After rinsing and drying, a technician grades the colour change of the fabric on the ISO 105-A02 grey scale and the staining of each fibre in the multifibre strip on the ISO 105-A03 scale, from 1 to 5. At home you can do a rough check by washing a garment with a white cloth, but only a lab report to a named method will settle a dispute with a supplier.
Why do dark colours fail rubbing tests more often?
A dark shade simply carries more dye, so any colour sitting loosely on the fibre surface shows up clearly on a white rubbing cloth. Testing both wet and dry matters, because a fabric can pass one state and fail the other. The colourant type matters too. Pigments sit on the fibre with a binder rather than bonding inside it, and vat and sulphur dyes can leave surface colour if they are not fully washed off. OEKO-TEX STANDARD 100 recognises this by accepting a dry rubbing grade of 3, rather than 4, for pigment, vat and sulphur colourants. The practical fixes are thorough washing-off after dyeing, correct fixation, and sometimes an after-treatment agreed with the dyehouse. For black denim, navy fleece or red cotton, ask for wet and dry rubbing results on the actual bulk dye lot before you approve cutting, not only on the lab dip.
What is colour fastness in clothing?
Colour fastness is how well a garment’s colour survives washing, rubbing, light, sweat and water without fading or staining other fabrics; ISO 105-A01 defines it as the resistance of a textile’s colour to the agents it meets during manufacture and use. Each test reports two results: change in colour, meaning how much the tested fabric itself faded or shifted, and staining, meaning how much colour moved onto an undyed adjacent fabric or rubbing cloth. Both are graded on grey scales from 1, severe change, to 5, no change, with half grades between, except light fastness, which uses a 1 to 8 blue wool scale. Other changes, such as shrinkage or a change in surface gloss, are reported separately. A report that says only pass, without both grades and the method number, is of little use.
What is the difference between ISO 105 and AATCC colour fastness tests?
ISO 105 and AATCC are two separate families of colour fastness test methods: the principle is the same but the procedures differ, so a result under one does not replace a test under the other. ISO 105 is the international series, while AATCC methods, titled colorfastness in US spelling, are often written into specifications by US buyers. The nearest pairs are ISO 105-C06 and AATCC TM61 for washing, ISO 105-X12 and TM8 for rubbing or crocking, ISO 105-B02 and TM16.3 for light, ISO 105-E04 and TM15 for perspiration, ISO 105-E01 and TM107 for water, and ISO 105-E03 and TM162 for chlorinated pool water. Neither family sets pass marks. Name the exact method and test code in your specification so the lab tests what your buyer expects.
How is colour fastness to rubbing (crocking) tested under ISO 105-X12?
Under ISO 105-X12, a crockmeter rubs a white cotton cloth over the fabric, once dry and once wet, and the colour transferred onto each cloth is graded on the ISO 105-A03 grey scale from 1 to 5. Gester, an instrument maker, summarises the key settings for ordinary fabrics as a downward force of 9 N, a 104 mm stroke and a 16 mm rubbing finger. The nearest US method is AATCC TM8. Both the dry and the wet result belong in your specification, because a fabric can pass one and fail the other. OEKO-TEX STANDARD 100 requires a dry rubbing staining grade of 4, or 3 for pigment, vat and sulphur colourants, and sets no wet rubbing limit, so the wet grade has to come from your own quality manual.
How is light fastness graded on the blue wool scale?
Light fastness is graded under ISO 105-B02 by exposing the fabric to a xenon arc lamp representing daylight (D65) alongside blue wool references and grading its fading against them. The standard allows two sets of references, 1 to 8, preferred in Europe, and L2 to L9, preferred in America, and states that results from the two sets are not interchangeable. On the European set, reference 1 has very low light fastness and reference 8 very high, and each step is roughly twice as fast as the one before, so the gap between grade 3 and grade 5 is about four times the exposure. A light grade of 4 is therefore not the same as a washing grade of 4. Chamber humidity also changes the result, so compare suppliers only when both labs used the same reference set and exposure conditions.
Which colour fastness test does swimwear need for chlorinated pool water?
Swimwear needs colour fastness to chlorinated pool water, tested under ISO 105-E03 at 50 or 100 mg/l of active chlorine, or under AATCC TM162 when a US buyer writes AATCC methods. The test measures how well the colour resists active chlorine; the same standard uses a lower 20 mg/l for beach robes. Light fastness under ISO 105-B02 matters too: it is most important for outerwear, swimwear and caps. ISO and AATCC set no pass marks, so write the method, the test code and a minimum grade for colour change and staining into your specification, and ask the lab to report grades rather than just pass or fail.
Which colour fastness tests does babywear need?
Babywear usually needs a saliva and perspiration fastness test, which OEKO-TEX STANDARD 100 adds for baby products with reference to DIN 53160, as well as its stricter Class I staining grades. Under the February 2025 limit values, Class I, baby, requires staining grades of at least 3-4 for water, 3-4 for acid and alkaline perspiration and 4 for dry rubbing, and a result of fast for saliva and perspiration. Class II, for skin-contact items, accepts 3 for water and does not require the saliva test. The saliva test simulates babies mouthing fabric and checks whether any colour transfers. OEKO-TEX grades staining only, so washing fastness and colour change still need limits of your own. If you sell kidswear, plan for these tests from the first lab dip.
Sources
Checked . Rules and figures change, so confirm anything that affects your pricing.
- ISO via iTeh Standards — ISO 105-A01:2010 preview, General principles of testing (definition of colour fastness, colour change and staining, other changes reported separately) (opens in a new tab)
- ISO via iTeh Standards — ISO 105-C06:2010 preview, Colour fastness to domestic and commercial laundering (S and M tests, steel balls, multifibre fabrics by temperature) (opens in a new tab)
- ISO via iTeh Standards — ISO 105-B02:2013 preview, Colour fastness to artificial light, xenon arc (D65 daylight, two blue wool reference sets) (opens in a new tab)
- James Heal — Grey Scale for assessing Staining, ISO 105-A03 (nine pairs of chips, grades 1 to 5 with four half steps) (opens in a new tab)
- OEKO-TEX — STANDARD 100 Limit Values and Individual Substances, Appendices 4 and 5, edition 02.2025 (colour fastness staining limits by product class, pigment, vat and sulphur exception) (opens in a new tab)
- OEKO-TEX — STANDARD 100 and ORGANIC COTTON Testing Methods, edition 01.2025 (ISO 105-E01, E04, X12 and DIN 53160 saliva test; staining only) (opens in a new tab)
- Gester Instruments — ISO 105-X12 Standard: Guidelines for Colour Fastness to Rubbing (force, stroke length, rubbing finger, grading with ISO 105-A03) (opens in a new tab)
- Cotton Incorporated — Chemistry of Fiber Reactive and Reactive/Disperse Dyes in the Printing Process, ISP 1015 (reactive dye bonding, washing-off, accelerated colour transfer check) (opens in a new tab)
- AATCC — PTP6 Colorfastness Proficiency Testing Program (AATCC TM8, TM15, TM16.3, TM61, TM107, TM133 and TM162 method titles) (opens in a new tab)
- ISO 105-E03:2010 via AFNOR — Colour fastness to chlorinated water (swimming-pool water): 50 and 100 mg/l active chlorine for swimwear, 20 mg/l for accessories (opens in a new tab)